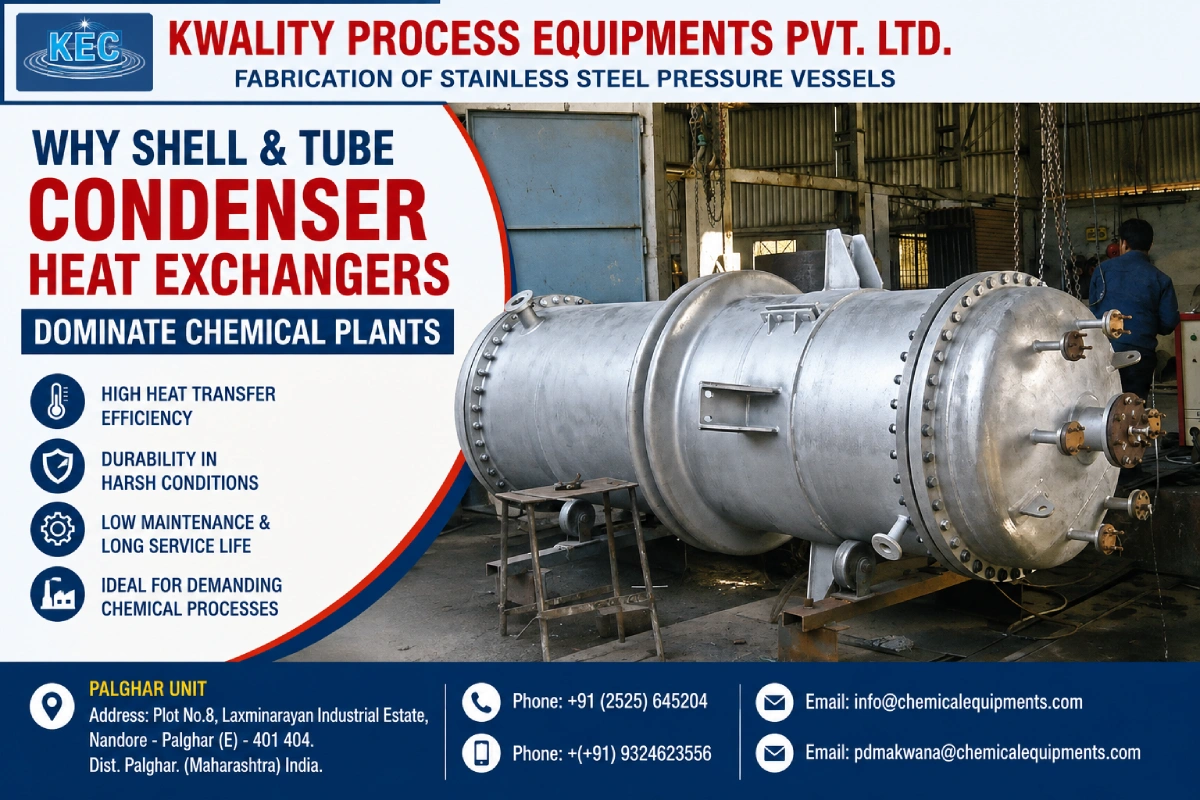
Why Shell & Tube Condenser Heat Exchangers Dominate Chemical Plants
In current times, any successful industrial chemical process relies heavily on the reliable performance of the condenser heat exchanger. Because it’s the ultimate key to successful heat management in chemical process industry plants. While traditional residential heating systems rely on simple technology, industrial facilities are required to use highly developed designs. To be capable of coping with corrosive vapors and aggressive liquids. Procurement specialists and plant engineers are always looking for equipment capable of providing maximum performance and adherence to strict international chemical industry standards. Choosing appropriate machinery implies taking into account the quality of construction materials and other details.
In order to increase the operational efficiency of your industrial facility, you need to choose an outstanding condenser heat exchanger design. As an excellent manufacturer of heat exchangers one need to provide you with products that outlive ordinary ones easily. By using high-quality stainless steel and other exotic alloys to outperform the traditional process. This blog explores the benefits of using shell and tube heat exchangers as well as the importance of selecting appropriate materials.
Different Types of Condensers Made by Heat Exchanger Manufacturer
Selecting the appropriate equipment format is absolutely vital for continuous petrochemical operations. Process engineers must carefully evaluate different configurations to ensure maximum thermal transfer and minimal maintenance downtime. This raises the need to partner with a heat exchanger manufacturer that understands this requirement and works towards it. Below is the comparison that highlights the primary industrial condenser types, detailing their specific operational strengths and ideal applications. To assist procurement managers in making highly informed, compliant purchasing decisions for modern chemical plants.
| Feature | Shell and Tube Condensers | Air Cooled Condensers | Vent Condensers |
|---|---|---|---|
| Primary Function | Handles massive liquid and vapor capacities | Cools chemical vapors using ambient air | Recovers toxic volatile compounds safely |
| Maintenance Needs | Requires periodic tube bundle cleaning | Needs routine fin inspection procedures | Demands minimal structural maintenance effort |
| Cost Efficiency | Highly cost effective for large plants | Reduces water consumption expenses greatly | Saves valuable materials from escaping |
| Material Options | Stainless steel and exotic alloy builds | Aluminum fins with robust steel tubes | High-grade anti-corrosive metal alloys |
| Industrial Usage | Dominates major fertilizer manufacturing facilities | Best for dry geographic plant locations | Essential for storage tank emission control |
| Space Footprint | Takes moderate industrial floor space | Requires significant external installation area | Very compact design for easy mounting |
| Thermal Rating | Provides superior heat transfer rates | Offers moderate thermal exchange efficiency | Highly specific to low volume flows |
| Lifespan Value | Long lifespan | Fair overall durability | High long-term |
Essential Advantages of Proper Material Selection
Designing a robust system for aggressive environments relies heavily on superior fabrication materials, and Kwality Process Equipments Pvt. Ltd. knows it. Chemical plants processing volatile acids, highly reactive fluids, or high-temperature solvents require equipment that rigorously avoids rapid degradation. Proper material selection effectively minimizes catastrophic mechanical failures and significantly reduces unplanned maintenance downtime during critical industrial operations. Here are the core operational benefits:
1. Superior Corrosion Resistance with Exotic Alloys
The use of top-quality materials, such as stainless steel, titanium, or special nickel alloys, offers protection against severe chemical aggression. Thus, prolonging the lifespan of all internal parts and the whole chemical processing machine under extremely tough conditions.
2. Compliance with Strict Chemical Industry Standards
The manufacturers ensure that each and every product adheres to stringent international standards for fabrication. This strict commitment ensures that the heavy-duty process is absolutely safe, completely compliant, and entirely optimized to maximize efficiency. The entire facility operation runs without any risk of fines or dangerous leaks of chemicals.
3. Simplified Maintenance and Tube Bundle Cleaning
The heat exchanger manufacturer develops the shell-and-tube design that prevails in the market. This allows access to clean the inside of the tubes in order to prevent fouling and scaling. Without the need to disassemble the entire system, thus saving tons of maintenance labor time each year.
4. Enhanced Thermal Efficiency and Pressure Tolerance
Selecting precisely engineered material ensures there will be no thinning of the walls under extremely high pressure. The structural strength of the heat exchanger maintains a constant rate of heat transmission, which cuts down energy costs. While working efficiently with the industrial volumes of fluid at all times of the year.
Choosing the right manufacturer of heat exchangers, such as Kwality Process Equipments Pvt. Ltd., ensures these critical factors are perfectly addressed. Our custom engineering solutions seamlessly integrate with different industries’ infrastructure, that help in delivering unmatched reliability. Across demanding fertilizer and petrochemical applications, ultimately boost your long-term return on capital investment.
Why is Kwality Process Equipments Pvt. Ltd. the Premier Choice?
While purchasing heat exchangers, choosing the best manufacturers plays a vital role next to designing. One such top-notch company that has made its reputation through its dedication to custom fabrications is Kwality Process Equipments Pvt. Ltd. Being different from general suppliers who ignore chemical engineering aspects, we know how important it is for a plant. Using extensive knowledge gained through decades of engineering experience, we manufacture condenser heat exchangers by carefully choosing high-end materials, which help you combat strong chemical corrosion.
- We offer you customized thermal engineering services so that each Condenser Heat Exchanger is built according to your spatial constraints and needs for heat exchange recovery. This way, your plant will avoid unnecessary bottlenecks when dealing with heavy processes.
- You get accurate metallurgical compatibility since your plant engineer knows the importance of material selection. Stainless steel, titanium, and alloys are used in manufacturing, which will resist aggressive corrosion and thermal stresses.
- The condenser heat exchangers are manufactured keeping maintenance efficiency in mind so that your maintenance team can clean up tubes effortlessly inside the system without causing plant shutdowns.
Wrapping It Up!
Upgrading your condenser heat exchanger is still an essential task that will determine the success of your chemical manufacturing operations today. The management has to ensure that the condenser heat exchangers used in their plants are made of the best quality. Using stainless steel and alloys so that they can handle extreme working conditions in their industries. In addition, using sturdy shell-and-tube designs helps manufacturers to maximize their heat recovery and minimize the complexity of maintenance work involved. Quality equipment plays an important role in the safety of processes and production.
Collaboration with a reputable industrial manufacturer is always sure to give you reliable results. With an old plant, upgrading to custom-built heat exchangers provides the best safety in operation. Kwality Process Equipments Pvt. Ltd., a top heat exchanger manufacturer, makes sure to deliver well-engineered products that meet all the standards required in the chemical industry. Ensure the safety of your petrochemical processes by installing high-quality systems today.
FAQs
They give an extremely robust structure, besides facilitating easy internal cleaning. This sturdy arrangement is capable of handling huge amounts of liquid, and is definitely the most robust one when it comes to heavy industrial processing.
Stainless steel and other rare metals such as titanium give the best protection against chemical corrosion. Selecting the right material will prevent early wear and tear and avoid any unexpected downtime.
Yes. As an acclaimed heat exchanger manufacturer, we can design customized thermal equipment as per your exact requirements. Our professional team designs materials as per your industrial needs to maximize process efficiency.
We manufacture highly robust chemical equipment for use in fertilizer, petrochemical, and pharmaceutical industries. Their fabricated equipment will last well under harsh conditions of industrial activities.
Definitely. All their units go through thorough tests and are strictly to international manufacturing standards, so you don’t have to worry about it.